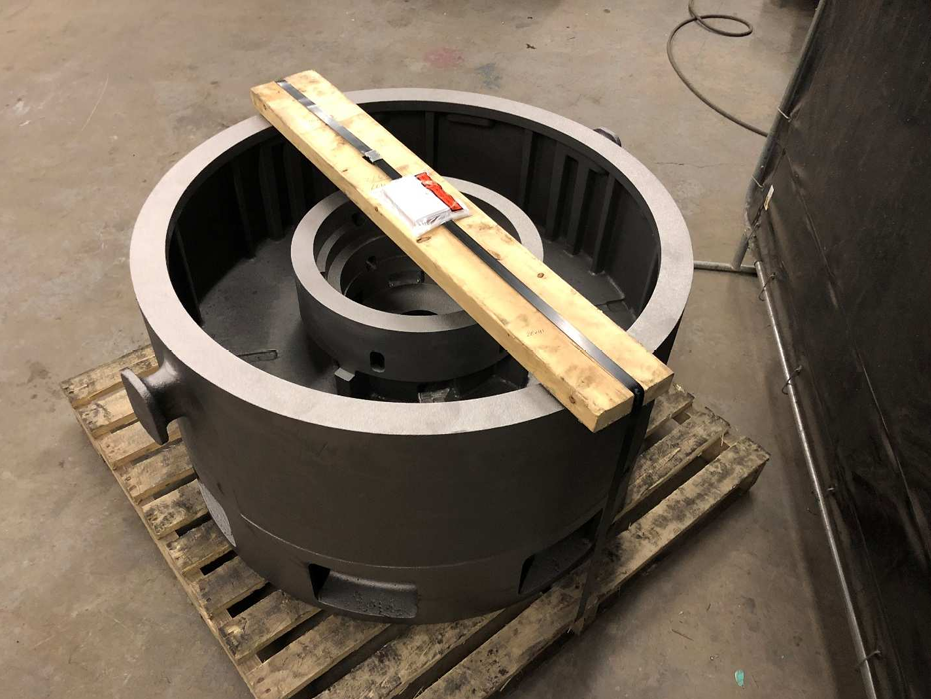
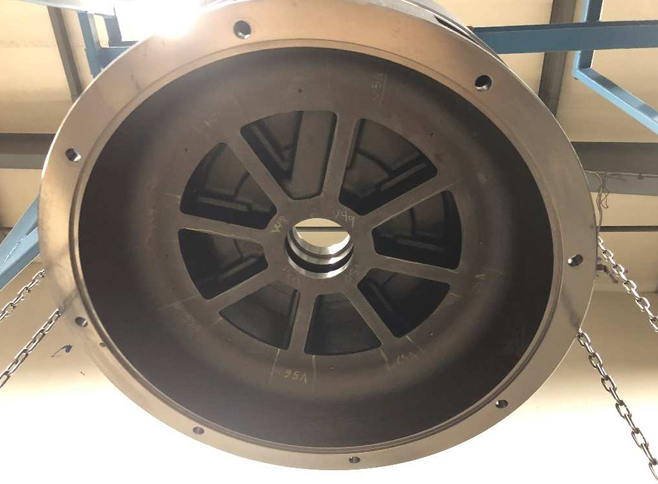
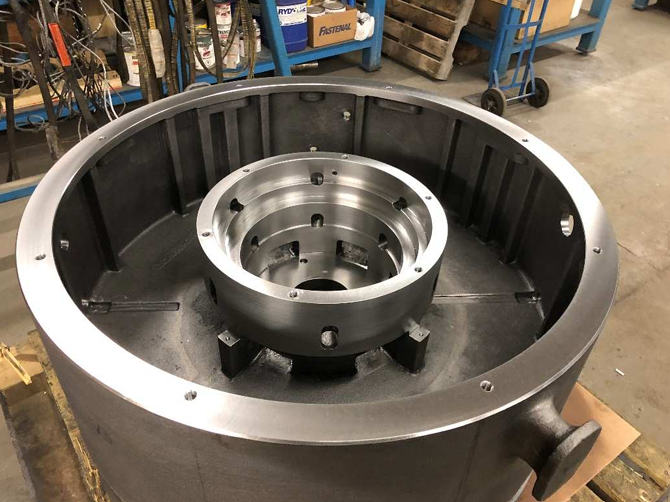
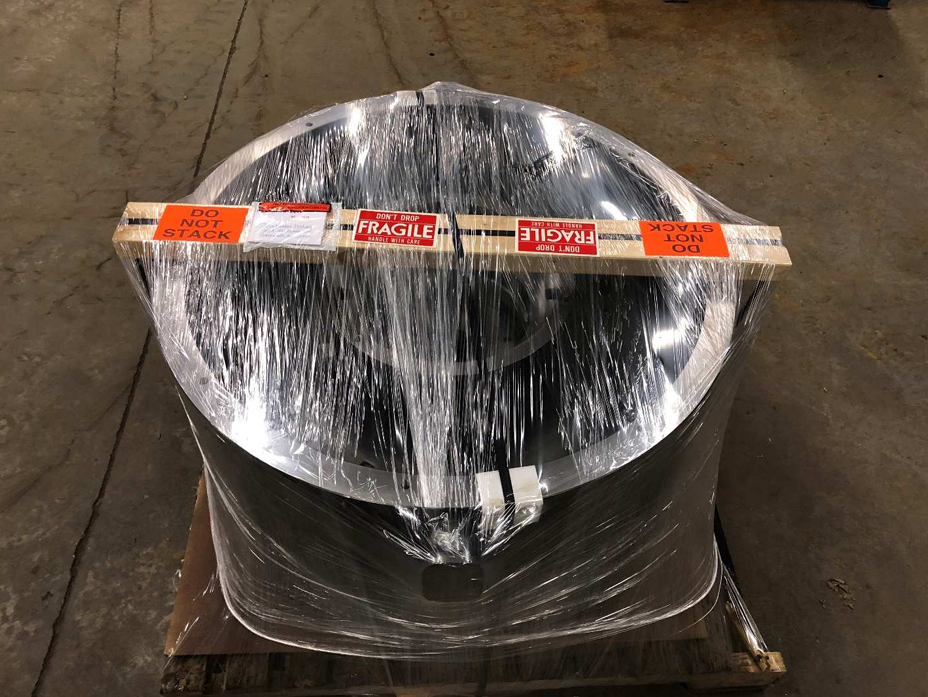
Siemens-Allis-Chalmers Nuclear Safety Motor Endbell
Project Date: 2017
Manufacturer: Siemens-Allis-Chalmers
Project Duration: 20 Weeks
Step 1:
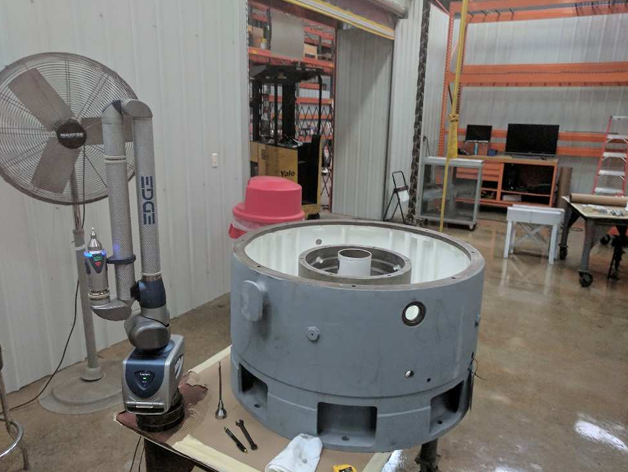
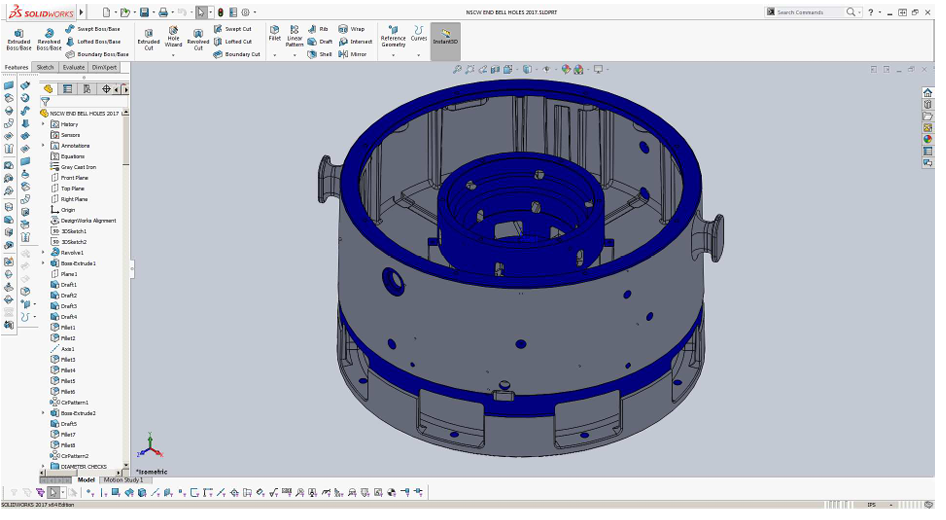
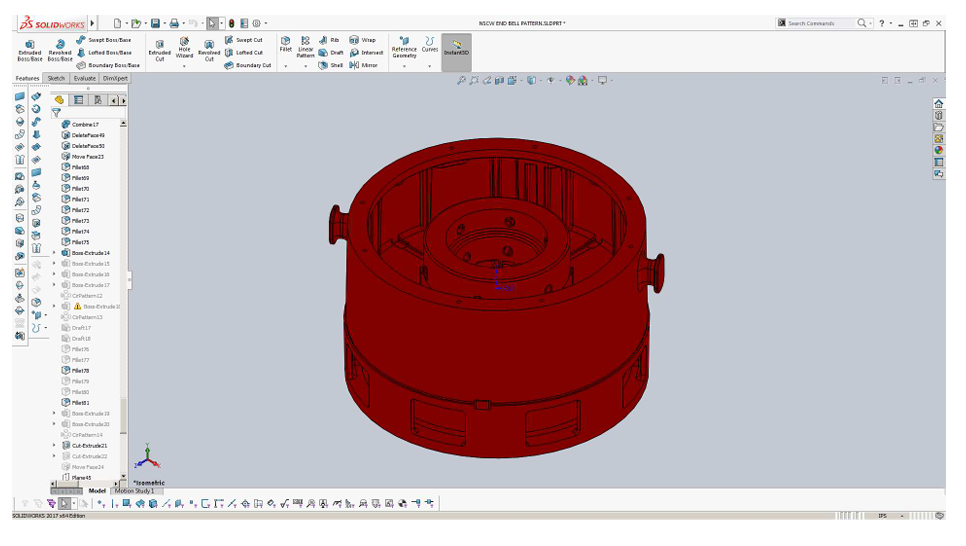
Measure original sample on-site using FaroArm Edge and Solidworks
Step 2:
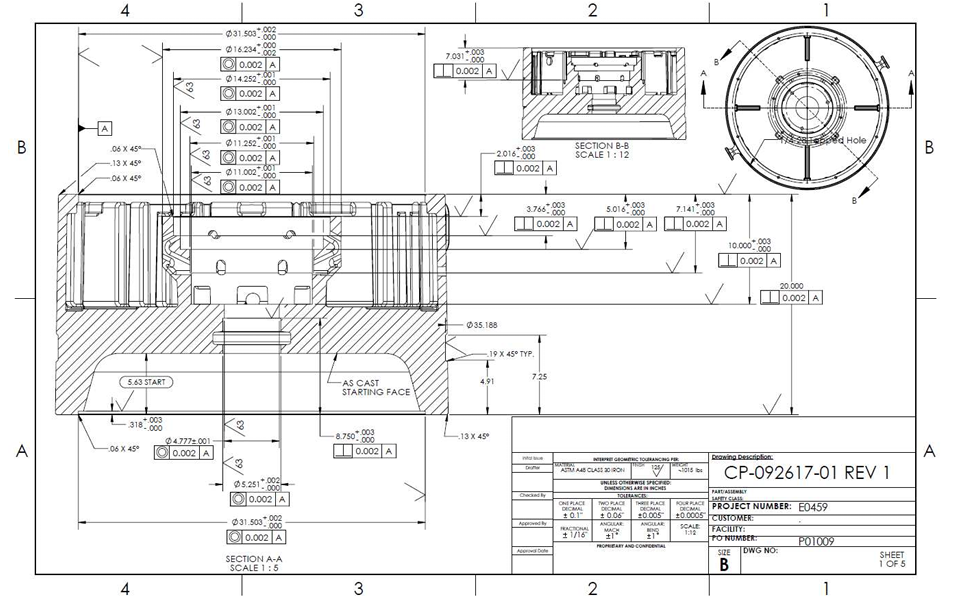
Once 3D CAD model is generated in Solidworks we create a machining drawing to be approved and finalized.
Step 3:
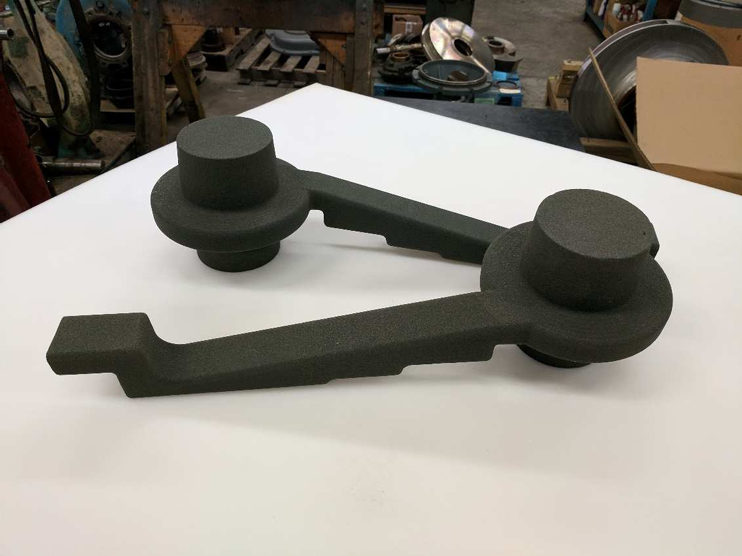
Once the machining drawing is finalized we add the required machining stock to the 3D CAD model which results in our casting model.
Step 4:
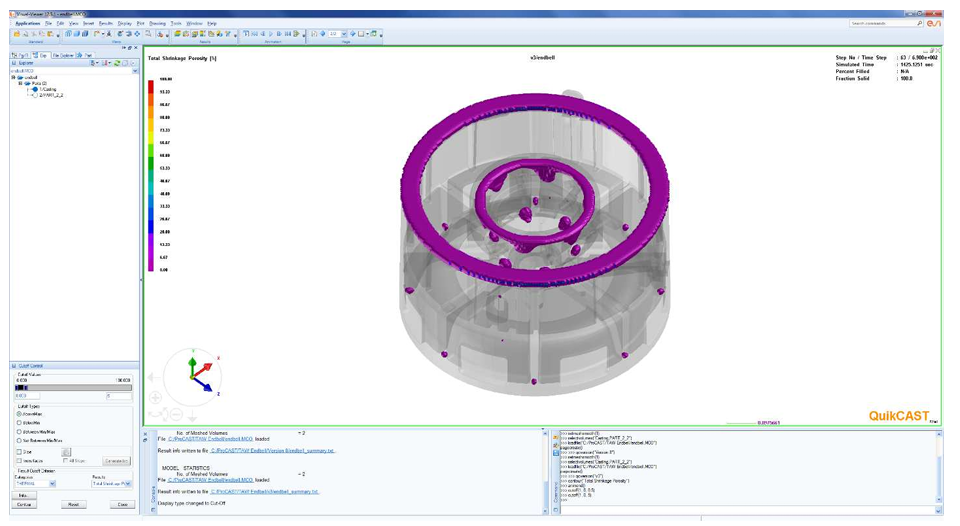
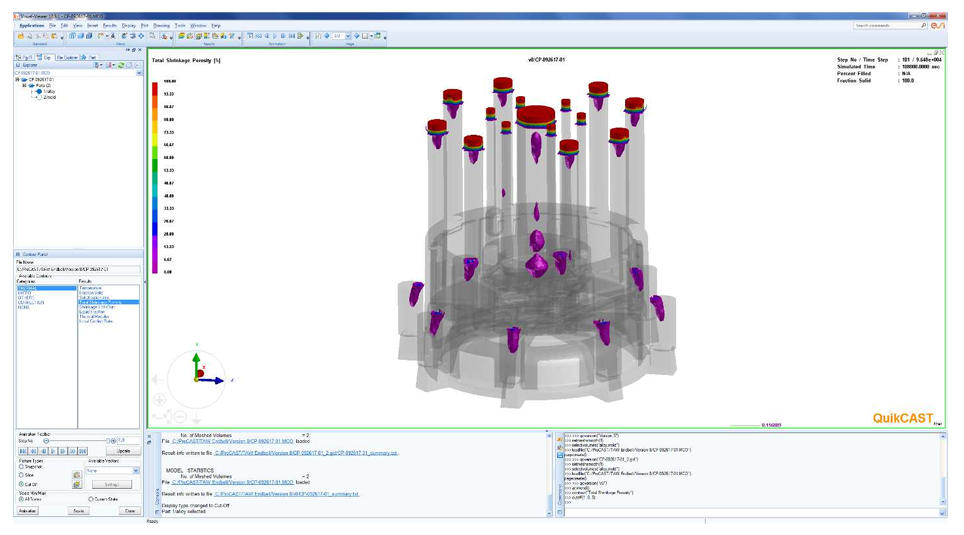
After the casting model is finalized we run multiple casting simulations in ESI QuickCast starting with no risers to identify problem areas and finishing with an optimized riser layout to ensure the casting is free of flaws.
Step 5:
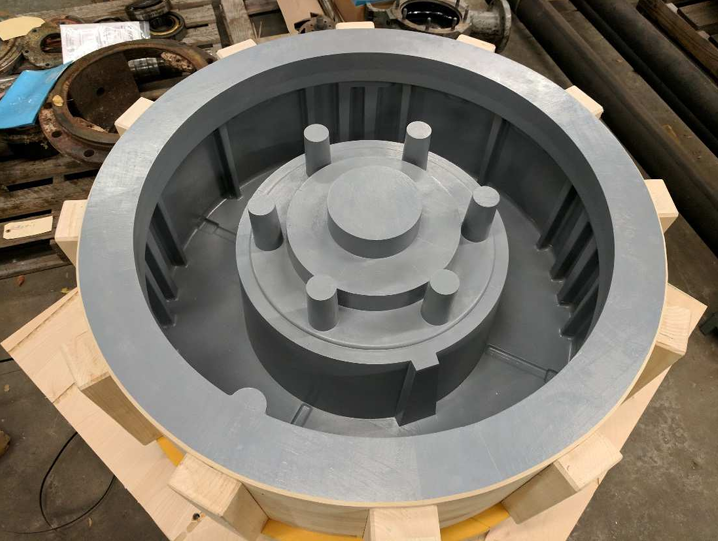
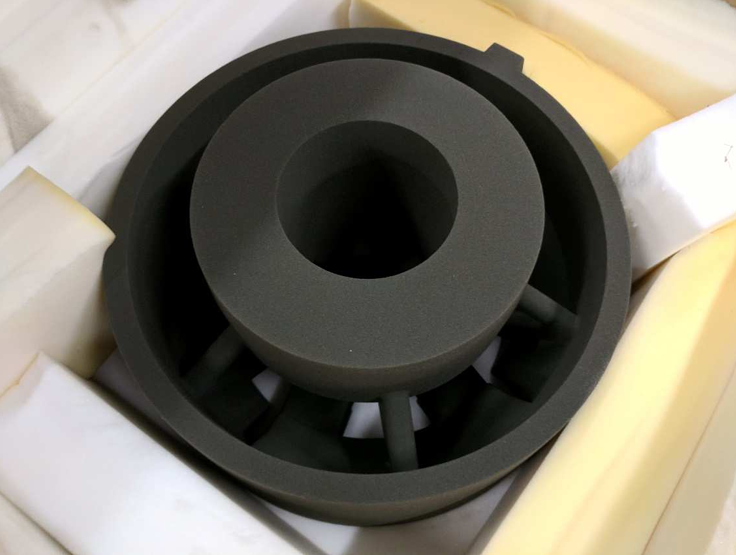
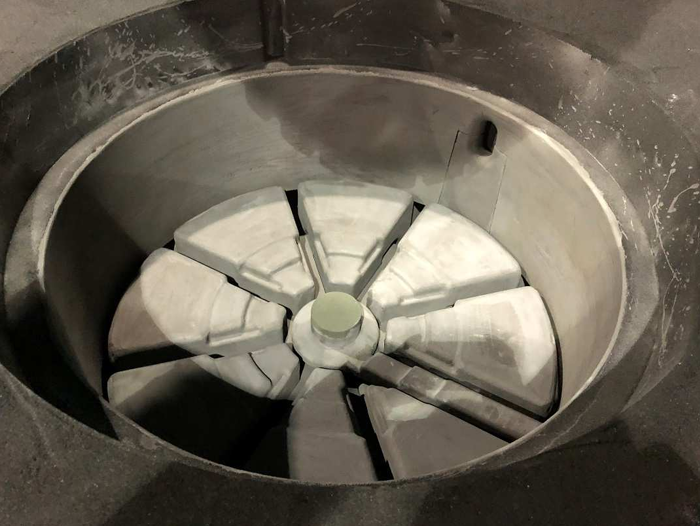
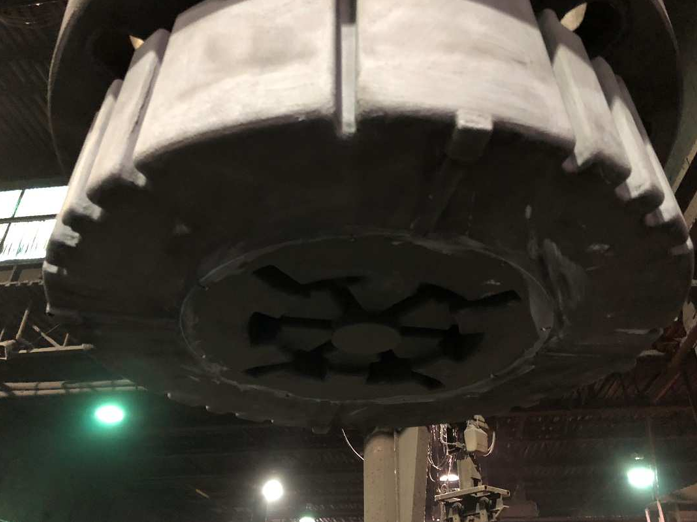
Once the layout is agreed upon by Emnor, the foundry and the tooling manufacturer the tooling is made. In this particular instance due to the complex geometry in the center of this casting it was decided to 3D print a sand core.
Step 6:
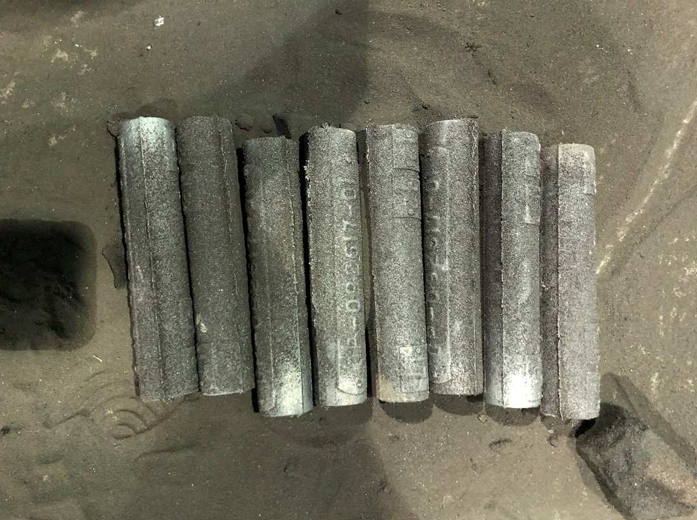
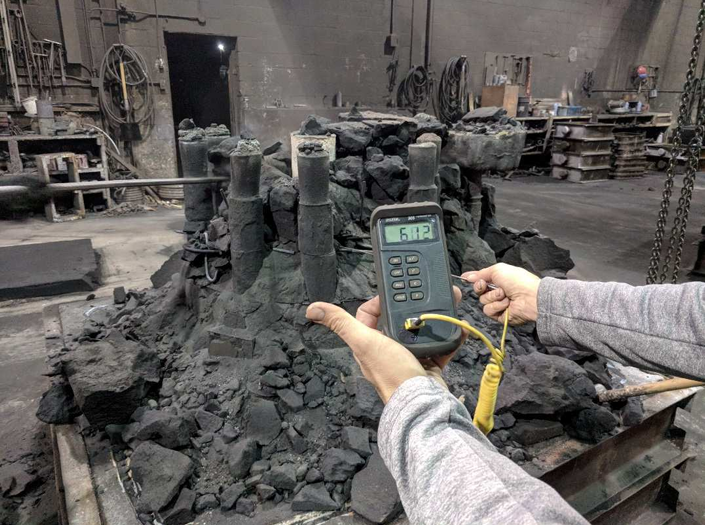
This project required the witnessing and video recording of the pour of the casting and the test bars. Test bars and casting were serialized.
Step 7:
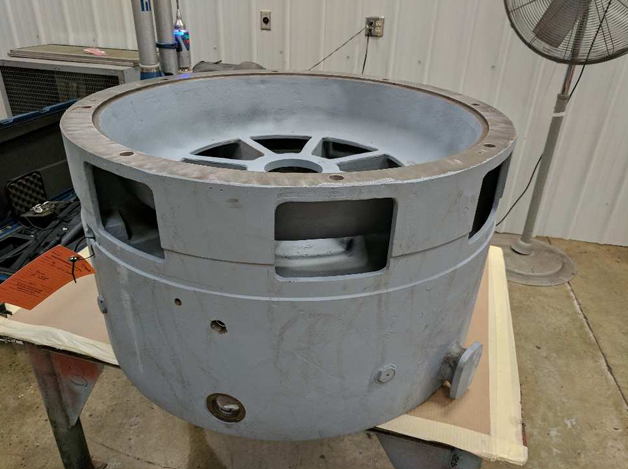
The test bars were sent from chemical and physical testing to a certified laboratory. Once positive results were received the casting was rough machined to remove the risers and sent for full X-Ray testing.
Step 8:
After passing X-Ray the casting was returned for final machining and sent for final X-Ray prior to customer delivery.